Soldering is a skill, and experienced engineers can often judge a board's quality at a glance. The defects below are the ones that show up most often on printed circuit boards, whether they come from hand soldering, rework or a production line. For each one, this guide covers what it looks like, why it matters and what typically causes it. Use it as a shared vocabulary between design, assembly and inspection teams.
Defects that break the electrical connection
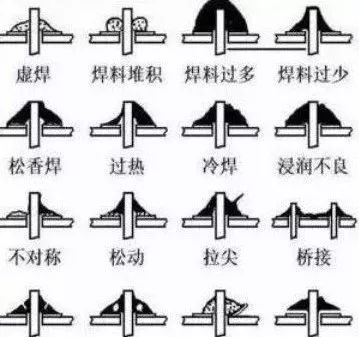
1. Cold or false solder joint (虚焊). A clear black boundary line appears between the solder and the component lead or copper foil, and the solder surface dips toward that line. The joint may not conduct reliably. Common causes: the component lead was not cleaned, not properly tinned or has oxidized; the board surface was not cleaned; or the flux applied was of poor quality.
2. Rosin joint (松香焊). Rosin residue is trapped inside the fillet. Strength is reduced and conduction can be intermittent. Causes include too much flux or flux that has lost its activity, insufficient heating time, or an oxide film that was never removed.
3. Loose lead (松动). The wire or component lead can physically move inside the joint. This leads to poor or open connection. It usually happens when the lead shifts before the solder solidifies, leaving a gap, or when the lead was poorly wetted or not wetted at all.
Defects in solder volume and shape
4. Excess solder (焊料过多). The solder surface is convex. It wastes material and can hide other defects underneath. Typically caused by withdrawing the iron too late.
5. Insufficient solder (焊料过少). The wetted area covers less than 80% of the pad and the solder does not form a smooth transition. Mechanical strength suffers. Causes: poor solder flow or early iron withdrawal, insufficient flux, or soldering time that is too short.
6. Solder accumulation (焊料堆积). The joint looks loose, white and dull. Mechanical strength is insufficient and a false joint may develop. Look for poor solder quality, soldering temperature that is too low, or lead movement while the solder is still molten.
7. Asymmetry (不对称). Solder does not flow across the full pad. Strength is reduced. Contributing factors are poor solder flow, insufficient or poor-quality flux, and inadequate heating.
8. Icicles and sharp points (拉尖). A pointed tip forms on the joint. It looks poor and can easily cause bridging to a neighboring trace. Often the result of too little flux combined with excessive heating time, or an improper iron withdrawal angle.
Wetting, overheating and bridging
9. Poor wetting (浸润不良). The contact angle between solder and workpiece is too large and the surface is not smooth. Strength is low and the connection may be open or intermittent. Causes: unclean parts, insufficient or poor-quality flux, or parts that were not heated enough.
10. Overheating (过热). The joint turns white, loses metallic luster and looks rough. Pads can lift and strength drops. This comes from an iron with too much power or heating applied for too long.
11. Cold solder joint (冷焊). The surface shows a grainy, tofu-like texture and may contain cracks. Strength and conductivity are both poor. The usual cause is vibration or movement before the solder solidifies.
12. Bridging (桥接). Solder connects two adjacent conductors that should be isolated. This is a direct short and one of the most damaging defects on fine-pitch parts. It is closely tied to excess solder, poor iron technique and insufficient flux activity.
Why these defects matter for inspection
Most of these failure modes are visible, which is why visual inspection and automated optical inspection (AOI) remain the first line of defense. But several of them, including false joints, loose leads and insufficient wetting, can pass a quick look and still fail in the field. That is why assembly flows combine visual inspection with X-ray inspection for hidden joints, cross-section analysis for suspect barrels and vias, and electrical test to confirm connectivity.
Process control matters as much as inspection. Solderability depends on board finish, storage conditions and handling. Surface finishes such as ENIG, lead-free HASL, immersion tin, immersion silver and OSP each behave differently during reflow and wave soldering, and the choice should match the component mix and the number of reflow cycles the board will see. Flux selection, preheat profile and iron temperature all interact with those choices.
Design choices that reduce risk
Many solder defects start in the design. Pad sizes that are too small for the component, thermal reliefs that are too weak, and tight trace width and spacing on fine-pitch devices all raise the probability of bridging and insufficient wetting. Running a design for manufacturability (DFM) review before panelization and stencil design is the cheapest way to remove those risks.
For through-hole assembly and mixed-technology boards, the interaction between stencil aperture design, solder paste volume and wave soldering parameters deserves early attention. A stencil that is well matched to the pad geometry reduces both excess solder and bridging, and it makes first article inspection (FAI) far more predictable.
What this means for your build
- Ask for the inspection plan up front: which defects are checked visually, which by AOI, which by X-ray, and where cross-section analysis is applied.
- Match your surface finish to the assembly process and reflow cycle count rather than defaulting to one option for every board.
- Review pad geometry, thermal reliefs and stencil apertures during DFM, before tooling is committed.
- Treat rework as a controlled process; hand soldering is where many cold joints, icicles and loose leads originate.
- Include electrical test and functional test in the flow so that intermittent joints are caught before the board ships.
Source: compiled from public web sources.